PCB Testing Methods: 8 Essential Techniques for Quality Assurance

PCB testing methods are the optical, electrical, and environmental checks used to find defects before a board ships. The eight common ones are AOI, ICT, flying probe testing, boundary scan, X-ray, functional testing, visual inspection, and burn-in. Choosing among PCB testing techniques means trading coverage against cost, speed, and fixture needs — AOI ICT flying probe testing sit at the front of that trade-off, with AOI catching surface faults fast, ICT delivering the deepest node coverage at volume, and flying probe testing keeping prototype runs affordable without a fixture.
Below, we break down each of the eight PCB testing methods: what it is, where it is used, and its advantages and disadvantages, plus why these checks still matter on a modern PCB manufacturing line.
1. AOI (Automated Optical Inspection)
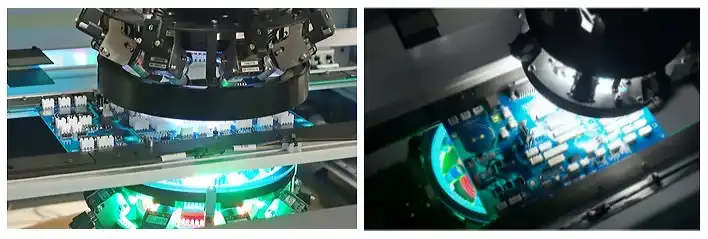
Taking top-and-bottom AOI. Images courtesy of MEK Marantz Electronics
AOI machines use high-resolution cameras to find surface-mounting errors. These errors include solder bridges, missing parts, and misalignment.
Scan after solder paste printing or reflow soldering in SMT assembly.
Advantage: Fast, non-contact, ideal for high-volume lines
Limitation: Cannot detect internal defects (e.g., voids)
Reference:
Automated Optical Inspection (AOI), Apps, and Machine Learning: Tools for PCB Quality Control
2. In-Circuit Testing (ICT)
ICT involves electrical probes that test individual components on a PCB assembly for shorts, opens, and component values.
Best for: Mass production, especially in rigid or flex-rigid boards
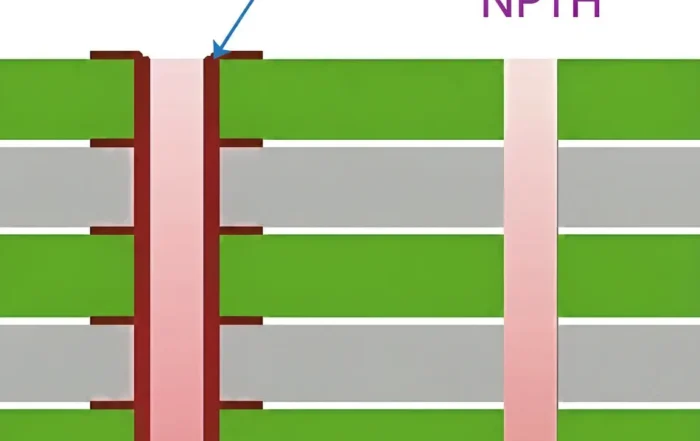
Tools: Bed-of-nails fixture, test access via PTH holes
Limitation: Costly fixture setup for small-batch runs
Reference:
How In-Circuit Tests Ensure PCBA Quality and Reliability
3. Flying Probe Testing
Flying probes work similarly to ICT but do not utilize a fixed test bed. They move across the board to check netlist connections and basic component values.
Advantage: Low setup cost, flexible for prototypes, and low-volume PCB assembly
Limitation: Slower than ICT; limited by access points
4. Boundary Scan (JTAG Testing)
For complex digital boards, boundary scan testing lets embedded parts test each other. You perform this through a serial test access port.
Application: BGA-heavy designs, high-density interconnect PCBs (HDI PCBs)
Advantage: Ideal for testing inaccessible areas
Limitation: Requires JTAG-compatible devices
Reference:
Boundary Scan Tutorial
5. X-ray Inspection (AXI)
Automated X-ray Inspection checks for hidden defects beneath BGA packages and inside multilayer PCBs.
Detects: Cold solder joints, voids, internal misalignments
Used in: Medical, military, and aerospace boards
Limitation: Expensive equipment; typically post-reflow
6. Functional Testing (FCT)
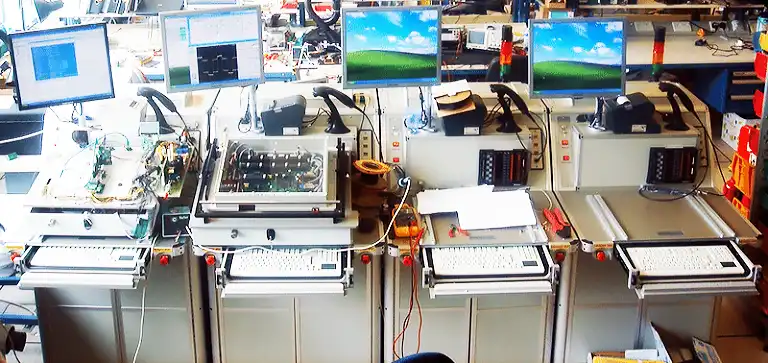
FCT Test
Functional tests simulate real-world conditions to validate board performance under load.
Benefit: End-to-end validation of assembled PCB
Used for: Final test phase before shipment
Tools: Custom test jigs, software simulators
Reference:
Functional Circuit Test (FCT) – A Basic Introduction Is Here – NextPCB
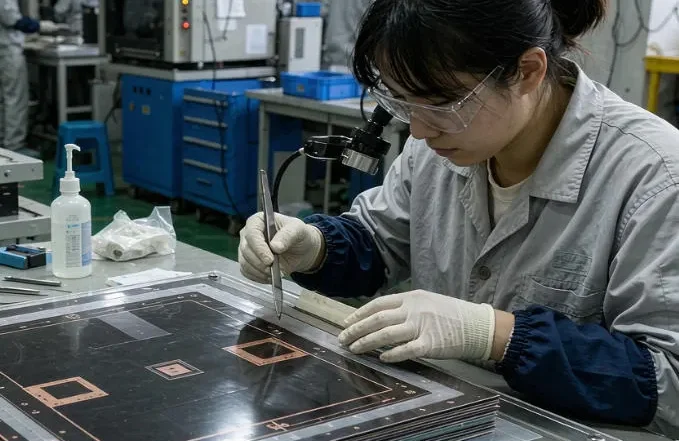
7. Visual Inspection
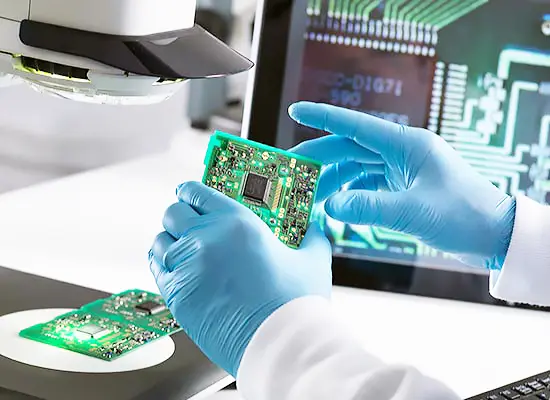
Visual Inspection
While basic, manual inspection still plays a role, especially for prototype PCBs, double-sided boards, and connector zones.
Used in: Low-budget setups or quick QA checks
Tips: Combine with checklists or smart magnification tools
Reference:
The essentials of manual visual inspection in PCB manufacture
8. Environment & Burn-In Testing
Burn-in involves running a board under stress conditions (high temp/load) to screen for early failures.
Used in: Automotive, military, or mission-critical applications
Test types: Thermal cycling, humidity, vibration, high-voltage
Test Flow and Yield Feedback Loop
A typical PCB test flow follows the manufacturing order:
“`
SPI → AOI → ICT / Flying Probe → Functional Test → Burn-in (if required)
“`
X-ray is inserted after reflow for BGA-heavy boards, and boundary scan may run alongside ICT. Each station generates data. The yield feedback loop collects first-pass yield (FPY) and defect data, analyzes root causes (e.g., paste printing issues, component placement errors), and feeds corrective actions back to the responsible process. This closed-loop approach reduces DPPM and improves overall yield.
Standards and Compliance
PCB testing often references IPC standards. IPC-A-610 defines acceptability criteria for electronic assemblies, while IPC-9252 covers electrical test requirements. For bare boards, IPC-6012 specifies qualification and performance. Military standards like MIL-STD-883 use grouped testing (e.g., Group A: electrical, Group B: mechanical, Group C: thermal, Group D: endurance) for qualification. In civil applications, full military qualification is rarely required, but elements such as thermal cycling, IST, and solderability testing are commonly adopted for automotive, medical, and industrial products. Automotive programs may follow AEC-Q100/Q200, which reference similar test methods. Always specify the applicable standard with your manufacturer.
Choosing the Right PCB Test Strategy
No single method covers every defect. Therefore, match the test to volume, board complexity, and reliability class. Keep one rule in mind: each method has a known blind spot, so stack them.
AOI, ICT and Flying Probe Testing: Quick Comparison
| Method | Cycle time (per board) | Setup/equipment cost | Fixture required | Best volume | Blind spot |
|---|---|---|---|---|---|
| AOI | 5–20 s | $50k–$200k (equipment) | No | High volume | Internal joints |
| SPI | 5–15 s | $40k–$150k (equipment) | No | High volume | Paste only |
| ICT | 10–30 s | $5k–$20k (fixture) + $50k–$150k (tester) | Yes | Mass production | Probe access |
| Flying probe | 30–120 s | <$1k (setup) + $80k–$200k (machine) | No | Prototype, low volume | Access points |
| X-ray (AXI) | 20–60 s | $100k–$500k (equipment) | No | BGA, multilayer | Cost and takt time |
| Boundary scan | 1–10 s | Low (software + JTAG port) | No | Dense digital boards | JTAG-compatible parts |
| FCT | 30–300 s | $2k–$50k (custom jig) | Yes (custom) | Final gate | Fault location |
| Burn-in | Hours | $10k–$100k (chambers) | Yes (sockets/boards) | High-reliability | Long cycle time |
Costs are rough industry ranges; actual figures vary by region and complexity.
Design for Testability
Design choices cut test cost before a single board is built. Add test pads and access holes so probes can reach critical nets. Keep JTAG chains on digital parts. In addition, reserve probing space on fine-pitch areas.
Talk to your manufacturer during layout. The PCB Manufacturing FAQ lists common review points, and Cleaning PCB Boards explains why residue causes false probe failures.
Coverage, Escape Rate and DPPM
Test coverage is the share of nets and components a test actually touches. Escape rate and DPPM track defects that reach the customer. Ask suppliers for both figures, not just a pass stamp. Also review process data, such as Multi-layer FPC manufacturing yields, when you audit a line.
Conclusion
Using the right testing strategy is essential. This applies whether you are making flexible FPC boards, high-speed HDI circuits, or standard single-sided assemblies. This helps ensure your products perform consistently.
Need help designing or validating your PCB test flow? Gekun provides end-to-end PCB solutions, from design to SMT to testing. Get in touch with our engineering team today.
FAQ:
1. Why is PCB testing important in modern electronics manufacturing?
As PCBs become more complex—with higher densities, fine-pitch components, and multilayer designs—testing is crucial to detect hidden defects, maintain stable manufacturing yields, and ensure the final product meets performance and reliability specifications. Effective testing reduces failures, returns, and field issues.
2. What is the difference between AOI and X-ray inspection?
AOI (Automated Optical Inspection) uses high-resolution cameras to detect surface defects such as missing components, solder bridges, or misalignment. It is fast and ideal for high-volume SMT lines.
X-ray inspection (AXI), however, can detect hidden or internal defects—such as voids, BGA solder issues, and internal misalignments—that AOI cannot see. AXI is more expensive and typically used for high-reliability boards.
3. When should I use In-Circuit Testing (ICT) vs. Flying Probe Testing?
Use ICT when:
You have mass production
Boards have accessible test points
You need fast, high-coverage testing
Use Flying Probe when:You are building prototypes or low-volume batches
You want to avoid high fixture costs
Your design changes frequently
ICT is faster but more expensive to set up; flying probe is slower but highly flexible.
4. What is Boundary Scan (JTAG), and when is it needed?
Boundary Scan (JTAG) allows embedded ICs to test interconnects through a serial interface. It is essential for:
HDI boards
BGA-dense layouts
Areas where test probes cannot reach
Its limitation is that all participating devices must support JTAG.
5. What is Functional Testing (FCT), and why is it used?
Functional Testing simulates real operating conditions to verify the fully assembled PCB behaves exactly as designed. It checks power-up behavior, signal response, interfaces, and safety requirements. FCT is typically the final test stage before shipment and helps catch faults that electrical or optical tests may miss.
6. What types of PCB tests are required for high-reliability applications?
Sectors such as automotive, aerospace, defense, and medical devices typically require:
AXI (X-ray) to check internal structures
Burn-in and environmental tests (thermal cycling, humidity, vibration)
FCT to ensure the board works under real-world load
These stress tests help identify early failures and ensure long-term reliability in mission-critical applications.
7. Should one line run AOI, ICT, and flying probe testing together?
Usually not all three on the same board. High-volume lines pair AOI with ICT, while prototype and low-volume builds swap ICT for flying probe testing to avoid fixture cost. Boundary scan then covers BGA-heavy designs where probes and cameras cannot reach the joints.
Related Posts
- Cleaning PCB Boards — Related article
- Inner-Layer Pad Protection Methods for FPC — Related article
- Multi-layer FPC Manufacturing Process: Cutting to Testing — Related article
- Nickel–copper adhesion failure in flexible PCBs | Causes & Fixes | Gekun — Related article
- PCB Hole Wall Quality Inspection: Methods, Criteria & Fixes — Related article