Rigid Flex PCB Manufacturing: A Step-by-Step Process
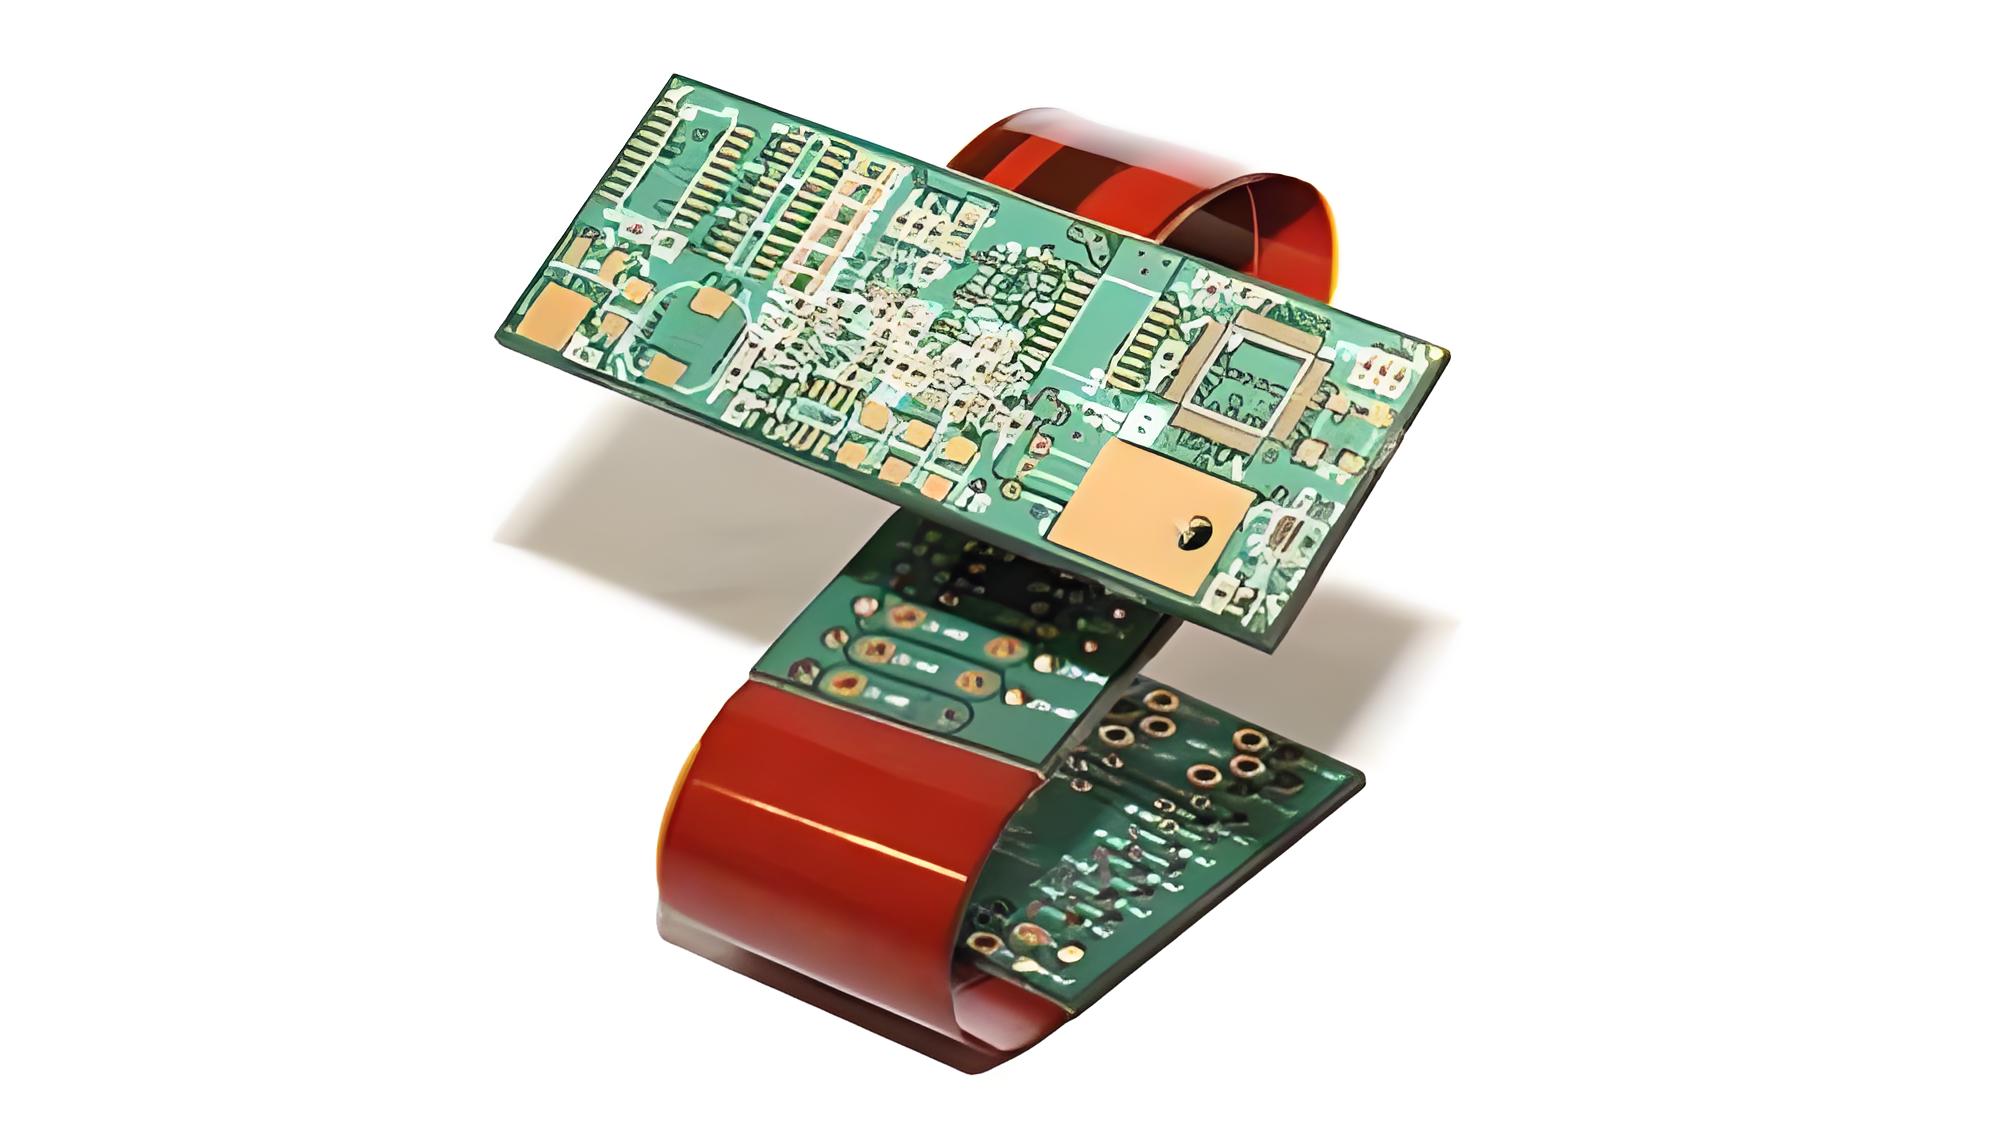
Therefore, rigid-flex PCB Manufacturing combines rigid FR4 sections with flexible polyimide circuits in one board. Additionally, the process is more complex and time-consuming than rigid board fabrication because flex zones, rigid zones, and transition zones each need separate control. Meanwhile, this guide follows an end-to-end flow: design input and DFM, material and stackup selection, inner-layer imaging, lamination, drilling and plating, outer-layer imaging, coverlay, surface finish, profiling, and test. For example, it also explains material choices, quality checks, defects, cost, and supplier selection.
In addition, see also Custom Flex PCB for related specifications.
As a result, see also Rigid-Flex PCB Technology for related specifications.
However, see also PCB Manufacturing FAQ for related specifications.
What Is a Rigid Flex PCB?
In practice, a rigid flex PCB is a printed circuit that contains both rigid and flexible sections in a single structure. Next, the rigid area carries components and connectors; the flex area bends or folds; the transition zone joins them. Consequently, one board can replace several rigid boards plus cables and connectors.
Flex PCB Classifications
Moreover, flexible circuits are classified by conductor layers and construction:
- Single-sided flex: one copper layer on polyimide.
- Double-sided flex: two copper layers with plated through-holes.
- Multilayer flex: three or more conductor layers bonded with adhesive or adhesive-less bondply.
- Rigid-flex: rigid FR4 layers combined with flexible polyimide layers.
- Semi-rigid flex: limited bending, often for assembly only.
In particular, FFC vs FPC: an FFC is a flat flexible cable made of parallel conductors, often used as a jumper; an FPC is a flexible printed circuit with etched copper traces, coverlay, and optional stiffeners. However, rigid-flex boards use FPC construction inside a rigid frame.
Rigid vs Flex vs Rigid-Flex
| Attribute | Rigid PCB | Flex PCB | Rigid-Flex PCB |
|---|---|---|---|
| Structure | FR4 only | Polyimide film with coverlay | FR4 rigid zones plus polyimide flex zones |
| Cost | Low to medium | Medium | High |
| Reliability | Good, but connectors add failure points | Good in bending, needs strain relief | High when transition zones are designed well |
| Applications | Most electronics | Wearables, cameras, thin devices | Medical, aerospace, automotive, compact handhelds |
Therefore, advantages of rigid-flex: fewer connectors and cables, space and weight savings, controlled impedance across the assembly, and higher reliability in motion. Additionally, limitations: higher fabrication cost, longer lead time, difficult rework, and strict DFM discipline at bend and transition areas.
The Rigid Flex PCB Manufacturing Process: End-to-End Overview
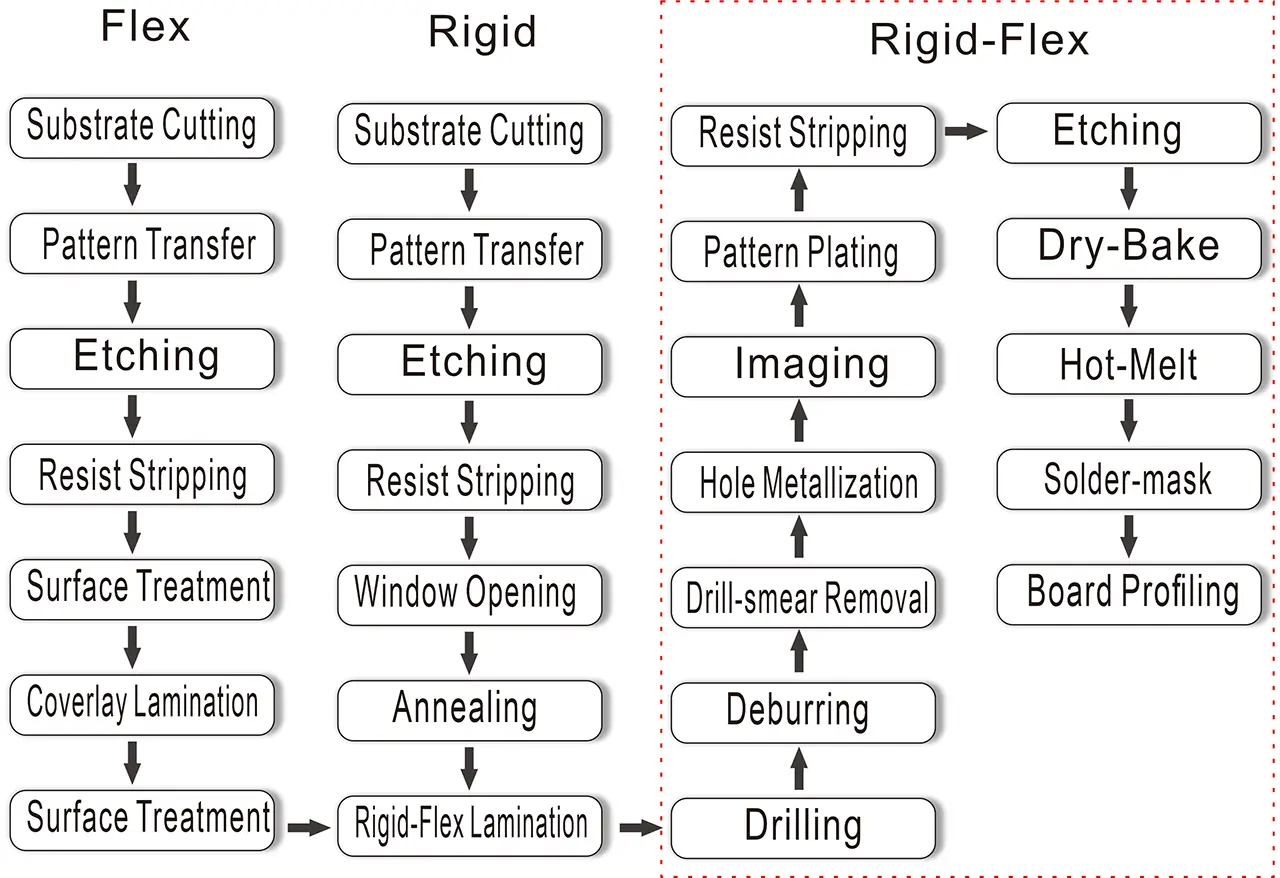
Rigid flex manufacturing process
Meanwhile, rigid-flex manufacturing carries more steps and more handling than rigid board fabrication. For example, flexible materials are thinner, more sensitive to moisture and scratches, and require separate imaging, lamination, and drilling settings. In addition, the process sequence is:
1. Design data and DFM review
2. Stackup and build-up planning
3. Material cutting and preparation
4. Inner-layer imaging and etching
5. Multilayer lamination
6. Drilling and plating
7. Outer-layer imaging and etching
8. Coverlay application
9. Surface finishing
10. Profiling and forming
11. Electrical and mechanical test
Each step feeds the next. As a result, a stackup error can appear later as warpage, coverlay misalignment, or a cracked copper trace.
Control Points by Zone
| Zone | Main control point |
|---|---|
| Rigid zone | FR4 thickness, layer count, flatness on the component side |
| Flex zone | RA copper bend endurance, polyimide thickness, coverlay bond |
| Transition zone | Tapered copper, microvia quality, CTE match, layer registration |
Design Inputs and DFM Rules That Affect Manufacturing
In practice, DFM decisions made before tooling determine yield and reliability. Next, for rigid-flex, the critical rules are:
- Bend radius: keep bends in the flex zone, not in the transition zone. Use a bend radius large enough for the copper type and layer count.
- Strain relief: avoid abrupt copper edges at rigid-flex junctions; use tapered copper and teardrops.
- Via placement: keep vias out of high-stress bend areas; use microvias in transition zones only when the stackup supports them.
- Layer alignment: design registration marks and allow for polyimide and FR4 movement during lamination.
- Coverlay openings: define openings for pads and connectors with enough clearance for coverlay flow and registration tolerance.
- Stiffener placement: add stiffeners under connectors or component areas that need local support.
Consequently, these rules must be reviewed with the fabricator before artwork is released. Moreover, design changes after lamination are expensive.
Material Selection and Stackup Preparation
In particular, material choice sets bend life, electrical performance, and cost. However, rigid-flex builds use polyimide flex cores, FR4 rigid cores, adhesive-less bondply or prepreg, coverlay, and stiffeners.
| Material | Role | Selection notes |
|---|---|---|
| Polyimide film | Flex base | 12–125 μm; high heat resistance; standard for dynamic flex |
| Adhesive-less FCCL | Flex copper clad | Removes glue layer; better dimensional stability and bend life |
| RA copper | Conductor in flex | Rolled annealed foil for bend endurance |
| FR4 | Rigid base | 0.2–3.2 mm; provides mechanical support |
| Bondply or prepreg | Adhesive layer | Controls flow, bond strength, and CTE match |
| Coverlay | Flex protection | Polyimide film with adhesive; protects traces and defines openings |
| Stiffener | Local support | FR4, polyimide, or metal for connectors and component areas |
| Surface finish | Pad protection | ENIG, OSP, or other finish selected for bend and assembly needs |
Therefore, high-volume production may use PET film for cost, but PET limits dynamic flex cycles. Additionally, for bending applications, use polyimide and RA copper. Meanwhile, adhesive-less FCCL removes the glue layer at flexible and rigid interfaces and improves CTE match. Stackup planning should balance layer count, flex thickness, and rigid thickness; asymmetric stacks are common but need CTE and warpage review.
Step-by-Step Rigid Flex PCB Manufacturing Process
Inner-Layer Imaging and Etching
Inner-layer circuits are imaged and etched on flex cores and rigid cores. Laser direct imaging supports fine traces on flexible printed circuit boards. Plasma etching can clean flex materials and control sidewall quality before lamination.
Multilayer Lamination
Lamination bonds flex cores, rigid cores, bondply, and prepreg into one panel. Flex prepreg bonding and rigid layer fusion use different temperature and pressure profiles. Lamination determines bond strength, coverlay registration, and warpage. Weak bonds show up later as delamination or bubbles.
Drilling and Plating
Laser drilling forms microvias in rigid-flex transition zones; mechanical drilling handles larger holes. Hole wall quality matters because flex materials smear differently from FR4. Electroless copper and electroplating build the copper thickness needed for reliable layers. Plating must cover transition-zone vias without cracking.
Outer-Layer Imaging and Etching
Outer layers are imaged and etched after lamination and plating. Registration to inner layers and to the flex openings is critical. Misregistration can reduce annular rings or short traces at the rigid-flex boundary.
Coverlay Application
Coverlay is the protective polyimide film that covers flex traces. It is laminated with adhesive and opened at pads, connectors, and test points. Coverlay misalignment is a common defect; it can expose traces or block pads. Proper coverlay design includes clearance, registration marks, and controlled adhesive flow.
Surface Finishing
| Finish | Cost | Bend cycles | Applications |
|---|---|---|---|
| ENIG | High | 200,000+ | Military and high-reliability flex |
| OSP | Low | 50,000 | Consumer flex and short-life assemblies |
Finish choice must match assembly, storage, and bend requirements. ENIG costs more than OSP and survives more bend cycles.
Profiling and Forming
Profiling cuts the board outline and separates rigid and flex areas. Laser or mechanical routing must avoid stress on flex traces. Forming may include bending or folding; fixtures and handling protect coverlay and copper from scratches.
Quality Control and Reliability Testing
Quality control covers electrical, mechanical, and visual checks. AOI inspects outer-layer patterns and coverlay openings. Flying probe or fixture test checks opens, shorts, and resistance. Four-wire Kelvin testing detects small resistance shifts. Impedance testing verifies high-speed traces, often within ±10%. Thermal shock and dynamic bend tests validate reliability.
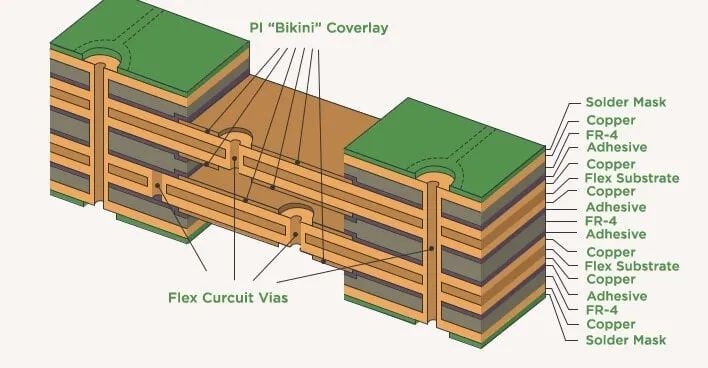
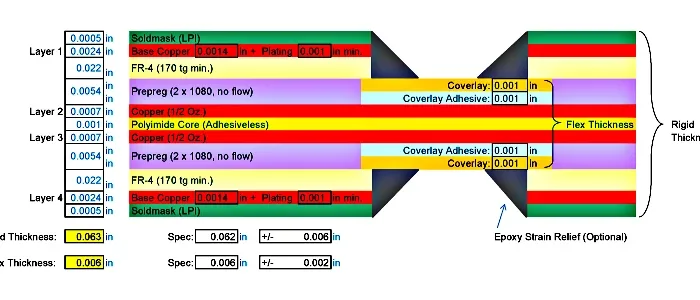
Rigid flex PCB stacked diagram
Mechanical validation may include:
- Dynamic flex test at a defined bend radius per IPC-2223C
- Thermal shock cycles from -55°C to 125°C
- Coverlay adhesion and hole wall inspection
Certification references commonly include IPC-6013D Class 3 for rigid-flex boards, UL 94V-0 flame rating, and ISO 13485 for medical devices. Buyers should request test reports for impedance, four-wire resistance, bend life, and thermal shock.
Common Defects and Troubleshooting
| Defect | Likely cause | Countermeasure |
|---|---|---|
| Delamination | Weak prepreg or bondply bond; moisture | Control lamination profile, dry materials, verify bond strength |
| Bubbles | Trapped air or volatiles in adhesive | Vacuum lamination, proper bake, adhesive flow control |
| Coverlay misalignment | Registration error or adhesive flow | Add registration marks, adjust coverlay size and lamination pressure |
| Poor hole wall quality | Smear or incomplete plating | Optimize drilling, plasma clean, control plating chemistry |
| Warpage | CTE mismatch and asymmetric stackup | Balance stackup, review CTE, control lamination cooling |
| Copper cracking | Sharp copper at bend or transition | Tapered copper, teardrops, larger bend radius |
Cost Drivers and Lead Time
Rigid-flex costs more than rigid or simple flex boards because it uses more materials and more process steps. Main cost drivers are material type, layer count, coverlay complexity, surface finish, yield, and test requirements. Prototype runs often use polyimide and RA copper with ENIG for reliability. Volume production may shift to lower-cost materials where bend life allows, but each change needs validation. Lead time is longer than rigid PCB fabrication because lamination, coverlay, and testing add steps and handling time.
How to Choose a Rigid Flex PCB Manufacturer
Check process control, not just price. A capable supplier documents transition-zone control, CTE data for each layer pair, lamination settings for flex and rigid bonds, and test reports for impedance, four-wire Kelvin, bend life, and thermal shock. Confirm certification coverage for the target market. Ask for DFM feedback before tooling and request samples or first-article reports for coverlay registration and hole wall quality.
Glossary: Rigid-Flex Terms
- Rigid-flex: a board with both rigid and flexible sections in one structure.
- FPC: flexible printed circuit with etched copper traces and coverlay.
- FFC: flat flexible cable made of parallel conductors; often a jumper, not a full circuit.
- Coverlay: protective polyimide film with adhesive that covers flex traces.
- Stiffener: local rigid material added under connectors or components.
- Bondply: adhesive film used to bond layers in flex and rigid-flex builds.
- Transition zone: the area where rigid and flex sections meet.
- RA copper: rolled annealed copper with high bend endurance.
FAQ
How does the rigid flex PCB process differ from rigid board fabrication?
It adds flex material handling, coverlay, and transition-zone controls. Flexible zones and rigid zones need separate imaging, lamination, and drilling settings. Transition zones need tapered copper, controlled layer registration, and microvia quality checks. Each board also passes bend and thermal shock tests before shipment.
Which rigid flex board quality standards apply?
Common references are IPC-6013D Class 3 for rigid-flex boards, IPC-2223C for dynamic flex testing, UL 94V-0 for flame rating, and ISO 13485 for medical devices. Buyers should request data for impedance, four-wire Kelvin resistance, thermal shock, and bend life.
When should a design use rigid-flex instead of flex or rigid?
Use rigid-flex when a product needs a stiff component area and a moving joint in one board. It removes connectors and cables, saves space, and improves reliability. Choose simple flex when there are no rigid component areas. Choose rigid boards when no bending is needed, and cost is the main driver.
What is the difference between FFC and FPC?
An FFC is a flat flexible cable with parallel conductors, often used as a jumper. An FPC is a flexible printed circuit with etched copper traces, coverlay, and optional stiffeners. Rigid-flex boards use FPC construction inside a rigid frame.
What are coverlay and stiffeners in rigid-flex manufacturing?
Coverlay is a protective polyimide film that covers flex traces and opens at pads. A stiffener is a local rigid piece added under connectors or components for support. Both affect registration, lamination, and final assembly.
How do design choices affect rigid-flex cost and lead time?
Bend radius, layer count, coverlay complexity, surface finish, and test requirements drive cost. Tighter bend radii and more layers need more process control. Prototypes take longer because lamination, coverlay, and testing add steps. Early DFM review reduces late changes and scrap.
Related Posts
- High-Frequency Rigid-Flex PCB Manufacturing — Related article
- Manufacturing Process of Semi-Rigid Flex PCB — Related article
- PCB Lamination Process | Rigid & Flexible PCB Manufacturing Guide — Related article
- Rigid-Flex PCB Manufacturing Guide — Related article
- HDI Rigid-Flex PCB Manufacturing for Medical Electronics — Related article