Flexible PCB Process Guide
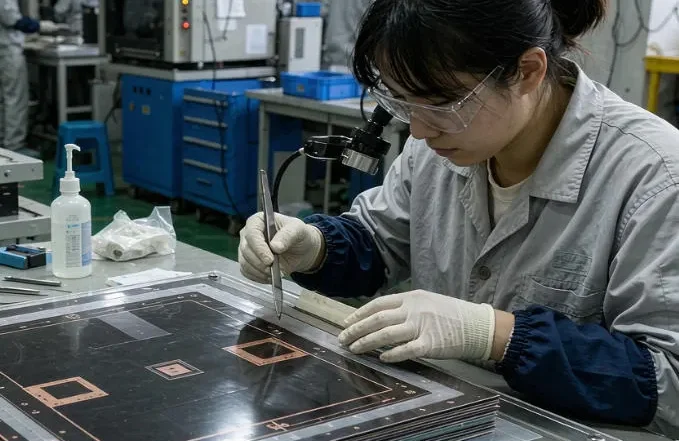
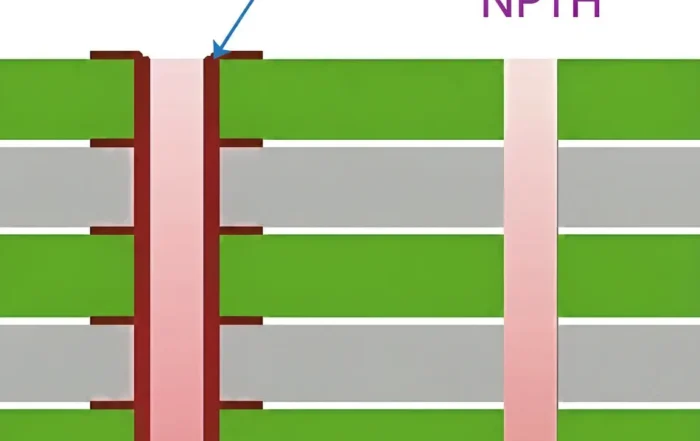
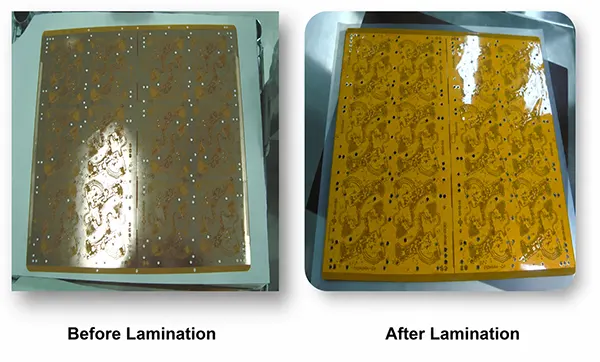
Therefore, this Flexible PCB Process Guide explains the FPC fabrication process step by step. Additionally, a flexible printed circuit is built on a polymer film, not on rigid fiberglass. Meanwhile, production runs through 11 controlled stages, from copper lamination and drilling to coverlay, surface finish and electrical testing. For example, each stage shapes conductivity, bend durability and long-term reliability. In addition, the sections below group the route by manufacturing stage and call out purpose, key control points, typical process windows and common defects. As a result, treat the windows as starting points; final settings must follow the material datasheet and the approved test plan.
In practice, see also Flexible Circuits for related specifications.
What Is an FPC?
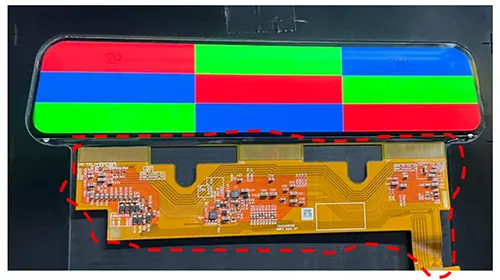
The FPC is marked with red dashed lines
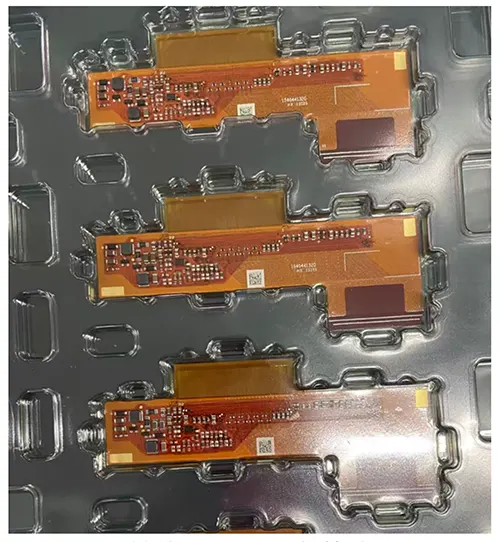
Single-unit FPC Tray disk loading
Next, FPC stands for flexible printed circuit. Consequently, it is a circuit built on a flexible polymer substrate, so it can bend, fold and fit tight spaces without losing electrical performance. Moreover, in a module drawing, the FPC is often the part marked with a red dashed box. In particular, before processing, single units are usually loaded onto trays, and black and white trays are common. As a result, the thin film stays flat and avoids creases during handling. A Flexible PCB therefore suits phones, automotive units, medical instruments, and wearables.
FPC Fabrication Process at a Glance
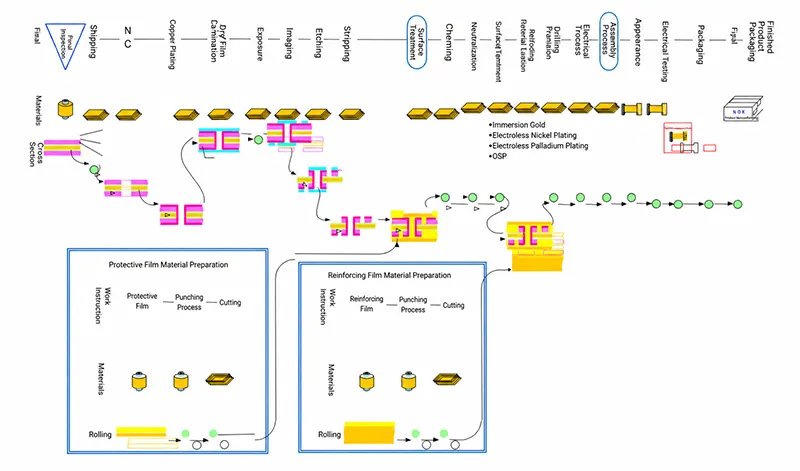
Overall FPC production process flow
Production Processes
However, for a double-sided flex board, the FPC fabrication process has 11 main stages. Therefore, the exact sequence varies from one manufacturer to another, so confirm the route with your supplier first.
1. Copper cladding
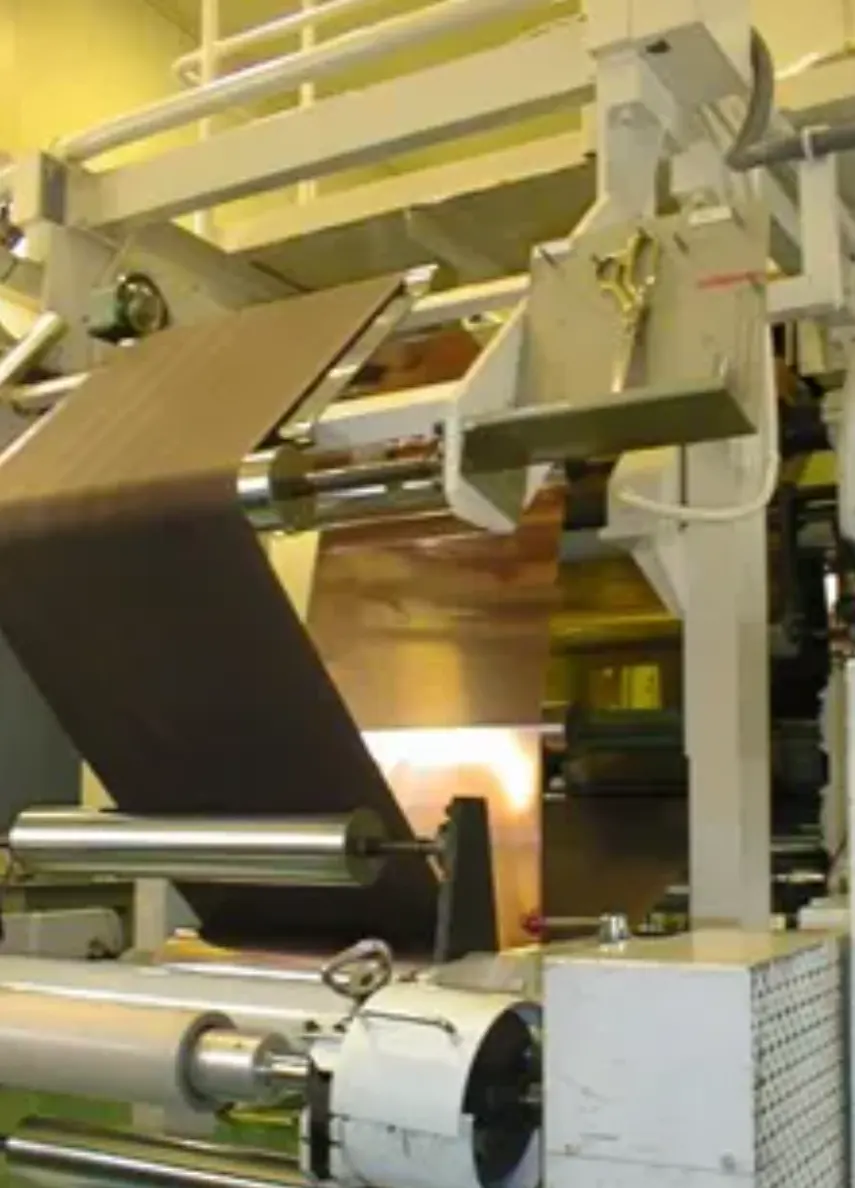
Copper Sheet
2. Die-cutting
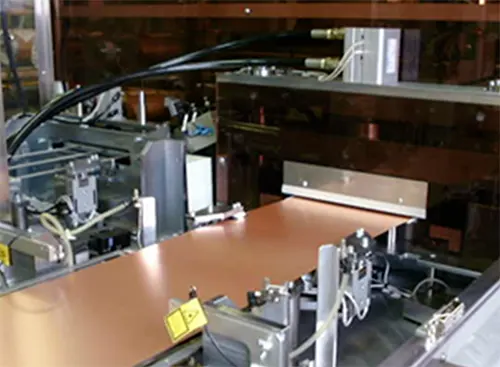
Cutting
3. Drilling
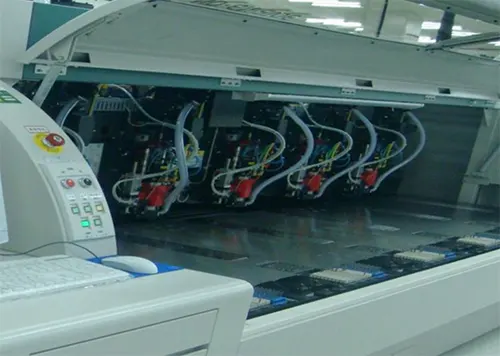
Drilling
4. Through-hole copper plating
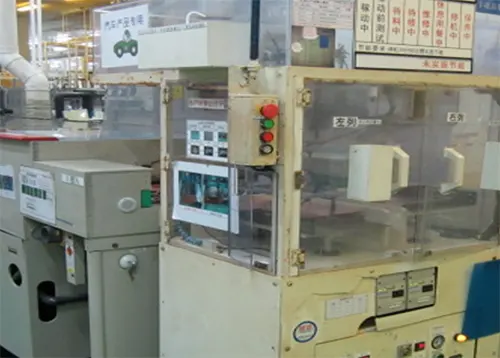
Copper plating at holes
5. Circuit formation
6. Coverlay lamination
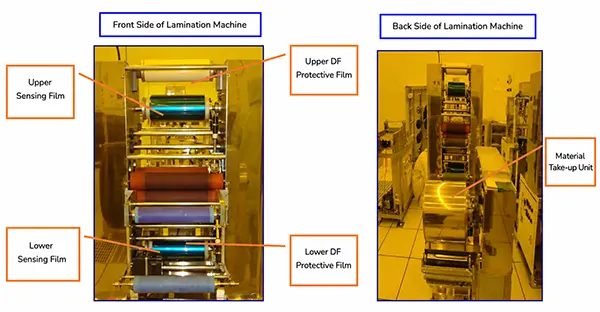
Dry film lamination
7. Curing
8. Surface treatment
9. Filler lamination and punching
10. Electrical testing
11. Inspection, packaging and shipping
Additionally, these 11 flexible PCB manufacturing steps form one continuous chain. Meanwhile, a fault at any stage, such as a weak plated hole or a shifted coverlay, shows up later in yield. For example, for process control, the same steps are commonly grouped into manufacturing blocks: material preparation and cutting, drilling and plating, pattern transfer, etching, lamination, coverlay, surface finish, forming, and electrical test.
Flexible PCB Build-Ups (Stack-Up)
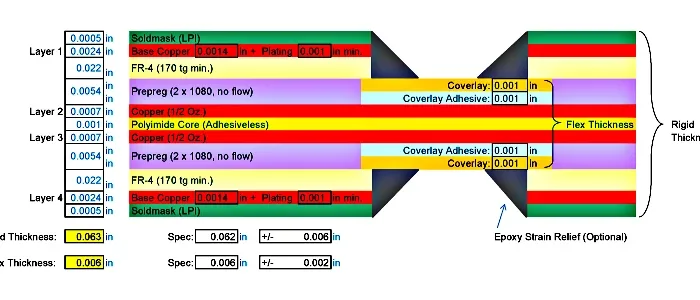
In addition, flex build-ups explain how the material layers are stacked, and the stack-up directly changes how the process is run. As a result, a simple single-sided flex build-up starts with base film, adhesive, copper foil, and a coverlay. In practice, a double-sided build-up adds a second copper layer and usually plated through-holes. However, a multilayer flex build-up repeats film, adhesive, and copper layers, so it needs more lamination cycles and tighter layer-to-layer registration. Next, a rigid-flex build-up combines flexible cores with rigid FR4 sections and often uses stiffeners or bonding layers at the transition zones.
Consequently, the stack-up affects process control in four practical ways. Moreover, first, adhesiveless laminates are thinner and give better flex life, but they demand cleaner handling and tighter etch control. In particular, second, thicker coverlay adhesive flows more during lamination and can squeeze into pad openings. However, third, more layers multiply lamination cycles and increase the chance of voids or delamination. Therefore, fourth, stiffeners and rigid-flex transitions create CTE mismatch, so forming and test must protect the bend zones. Additionally, mark every coverlay opening, stiffener zone and bend area on the drawing before release.
Material Selection: PI vs PET vs Thin FR4
| Option | Strength | Limit | Typical use | Process note |
|---|---|---|---|---|
| Polyimide (PI) | High heat resistance, good dimensional stability, strong flex fatigue life | Higher cost, moisture uptake | Dynamic flex, automotive, medical, industrial | Bake when needed, plasma clean, control lamination temperature and pressure |
| PET | Low cost, good clarity, good for static bend | Lower heat resistance, lower flex endurance | Static flex, displays, low-cost consumer parts | Keep lamination and cure below the material limit |
| Thin FR4 | Rigid support, low CTE, good for stiffener areas | Not for dynamic bending | Stiffeners, rigid-flex rigid sections | Route and bond as a stiffener, watch CTE mismatch at transitions |
Meanwhile, adhesive system choice matters as much as the base film. For example, an adhesive-based laminate is lower cost and easier to laminate, but the adhesive adds thickness, can flow into openings and may reduce dynamic flex life. In addition, an adhesiveless laminate is thinner, supports finer lines and gives better flex endurance, but it costs more and needs tighter handling and plasma treatment. As a result, use adhesive systems for static bend and cost-sensitive builds; use adhesiveless for dynamic bend, fine pitch and high-reliability designs.
Material Preparation and Cutting
In practice, the purpose of material preparation and cutting is to release the correct base material, bring it to panel size and stabilize it before imaging. Next, key control points are material type, film thickness, copper thickness and profile, adhesive system, lot traceability, cut tolerance, edge burr, fiducial placement and moisture control. A typical cut tolerance is plus or minus 0.1 to 0.2 mm, with burr kept under about 50 micrometres. When polyimide has absorbed moisture, bake it at about 120 to 150 degrees C for 1 to 4 hours before lamination or coverlay. Common defects are edge burr, scratches, creases, wrong material, dimensional error and moisture blister.
Drilling and Through-Hole Plating
The purpose of drilling is to create tooling holes and through-holes at programmed coordinates; plating then builds electrical continuity between copper layers. Key control points are drill bit diameter and wear, spindle speed, entry and exit material, hole position, hole wall quality, desmear or black hole treatment, plating thickness and hole wall coverage. A typical hole position tolerance is plus or minus 25 to 50 micrometres, and plated copper is often 20 to 25 micrometres, confirmed against the design. Common defects are hole wall cracks, plating voids, resin smear, open circuits and intermittent connections.
Pattern Transfer (Photolithography)
The purpose of pattern transfer is to define the conductor pattern in photoresist so that etching removes only the unwanted copper. Key control points are resist lamination temperature, exposure energy, artwork registration, development time and cleanliness. A typical resist lamination window is about 90 to 110 degrees C, with layer-to-layer alignment at plus or minus 25 to 50 micrometres. Exposure energy must follow the resist datasheet. Common defects are shorts, opens, resist residue, misregistration, undercut and damaged fine lines.
Etching
The purpose of etching is to remove exposed copper and leave the designed trace pattern. Key control points are etchant chemistry, etchant temperature, line speed, etch factor, rinse quality and trace width measurement. A typical cupric or alkaline etch bath runs at about 45 to 55 degrees C, and trace width should stay within plus or minus 10 percent or plus or minus 25 micrometres, whichever is agreed. Common defects are over-etch, undercut, residual copper shorts, etchant residue and trace width drift.
Lamination and Layer Bonding
The purpose of lamination is to bond multilayer layers, stiffeners or bonding sheets into a stable stack-up. Key control points are vacuum level, temperature ramp, pressure, dwell time, cooling under pressure and adhesive cure. A typical vacuum lamination window is about 160 to 190 degrees C at 1 to 3 MPa, with ramp and cool rates set by the adhesive datasheet. Common defects are delamination, voids, adhesive squeeze-out, resin starvation, warp and trapped air.
Coverlay Lamination and Curing
The purpose of coverlay is to protect traces, define the bend zones and open pads for assembly. Key control points are coverlay alignment, adhesive flow, lamination temperature and pressure, cure profile and opening cleanliness. A typical coverlay alignment is plus or minus 50 to 100 micrometres, laminated at about 150 to 170 degrees C and 0.5 to 2 MPa, followed by a staged cure. Common defects are coverlay shift, bubbles, lifted edges, adhesive squeeze-out, blocked pads and creases.
Surface Finish
The purpose of surface finish is to protect exposed copper pads and keep them solderable. Key control points are pretreatment, bath chemistry, temperature, dwell time, thickness and rinse. For ENIG, a typical target is 3 to 6 micrometres of nickel and 0.05 to 0.1 micrometres of gold. OSP and immersion tin are also common on flex. Common defects are skip plating, contamination, poor solderability, nickel corrosion and finish thickness out of range.
Forming and Singulation
The purpose of forming is to cut the panel into final outlines, open bend reliefs and singulate parts without damaging conductors. Key control points are tool wear, laser or die cutting parameters, cut tolerance, edge burr, radius control and handling support. A typical cut tolerance is plus or minus 0.1 mm, with no micro-cracks at the edge. Common defects are burrs, edge cracks, dimensional error, creases and damaged coverlay at the cut line.
Electrical Test and Inspection
The purpose of electrical test is to screen opens, shorts and isolation failures before shipment. Key control points are fixture accuracy, test voltage and current, resistance threshold, probe contact and test coverage. Use IPC-6013 as the qualification and performance reference for flexible printed boards, and use IPC-TM-650 test methods for peel strength and flexural endurance where the test plan calls for them. A bend test should state the bend radius, cycle count and acceptance rule in the approved test plan. Common defects are open circuits, shorts, intermittent contacts and false failures from fixture setup.
Key Process Windows and Acceptance Criteria
| Stage | Typical window | Acceptance check |
|---|---|---|
| Cutting | Cut tolerance plus or minus 0.1 to 0.2 mm; burr under 50 micrometres | Dimensions, edge quality, material lot |
| Drilling and plating | Hole position plus or minus 25 to 50 micrometres; plated copper 20 to 25 micrometres | Hole wall coverage, plating thickness, continuity |
| Pattern transfer | Resist lamination 90 to 110 degrees C; alignment plus or minus 25 to 50 micrometres | Resist resolution, registration, development |
| Etching | Etchant 45 to 55 degrees C; trace width plus or minus 10 percent or plus or minus 25 micrometres | Trace width, shorts, undercut, residue |
| Lamination | 160 to 190 degrees C at 1 to 3 MPa | Bond strength, voids, delamination, warp |
| Coverlay | Alignment plus or minus 50 to 100 micrometres; 150 to 170 degrees C at 0.5 to 2 MPa | Opening position, bubbles, adhesion, cure |
| Surface finish | ENIG Ni 3 to 6 micrometres, Au 0.05 to 0.1 micrometres | Thickness, solderability, contamination |
| Forming and test | Cut tolerance plus or minus 0.1 mm; bend test per approved plan | Outline, burr, continuity, bend result |
Defect and Countermeasure Table
| Defect | Likely stage | Countermeasure |
|---|---|---|
| Delamination | Lamination, coverlay | Check vacuum, ramp rate, pressure and cure; confirm adhesive shelf life and moisture bake |
| Blistering | Material prep, lamination, coverlay | Bake PI before processing; control moisture, lamination temperature and trapped air |
| Adhesive squeeze-out | Coverlay, lamination | Reduce pressure or flow, adjust coverlay opening, stage the cure and check adhesive thickness |
| Creases | Cutting, handling, forming | Keep single units on trays, reduce manual handling, support the film at every transfer |
| Coverlay shift | Coverlay | Improve registration, use fiducials, check lamination shrinkage and artwork compensation |
| Over-etch or undercut | Etching | Control bath temperature, line speed and etchant strength; monitor trace width |
| Hole wall cracks | Drilling, plating | Check drill bit wear, spindle speed and plating coverage |
Flexible PCB Manufacturing Steps vs Rigid PCB Process
The steps look familiar, yet the substrate changes how each one is run.
| Area | Rigid PCB | Flexible PCB |
|---|---|---|
| Substrate | Rigid glass epoxy | Flexible polymer film |
| Conductor protection | Solder mask | Coverlay film with adhesive |
| Handling | Flat panels | Trays for single units |
| Main risk | Warpage | Creases, coverlay shift, hole wall cracks |
Before you release a job, run this short check:
- Confirm the stack-up and copper thickness.
- Mark stiffener and coverlay zones on the drawing.
- Check bend areas for trace direction and coverlay openings.
- Agree on the test method and acceptance rules.
- Approve a sample before mass production.
A DFM review at this point cuts scrap and shortens the ramp from prototype to volume.
Yield, Cost and Prototype-to-Volume Transition
The main cost drivers in flexible PCB production are material choice, layer count, coverlay complexity, lamination cycles, surface finish and test coverage. Material and coverlay often dominate bare-board cost, while lamination and coverlay defects dominate scrap. Yield has a direct effect on cost per good unit: if yield moves from 85 percent to 95 percent at the same material price, cost per good unit falls by about 10.5 percent, because 0.85 divided by 0.95 is about 0.895. That is why coverlay alignment, lamination voids and etch control deserve SPC before volume release.
Use a staged transition from prototype to volume. Prototype runs are typically 1 to 50 pieces and focus on build-up, coverlay fit and bend performance. Pilot runs are often 50 to 500 pieces and should lock the process windows, test fixture and acceptance limits. Volume runs above 500 pieces should use controlled lamination and etch charts, incoming material checks and regular bend or peel tests. Freeze the stack-up, artwork and test plan before volume tooling, because late changes in coverlay openings or stiffener zones reset the learning curve.
Working with a Flexible PCB Manufacturer
Gekunflex is a Flexible PCB Manufacturer serving mobile, consumer, medical, automotive and industrial programs. Single-sided, double-sided, multilayer and rigid-flex builds all follow the controlled route above. For bend-critical parts, review High-Reliability Flexible Circuits for High-End Applications. For assembly after fabrication, see the Flexible PCB SMT process guide. Send your data and test plan, and we will confirm the route and quote. General questions are answered in the PCB Manufacturing FAQ.
FAQ
What are the flexible PCB manufacturing steps?
For a double-sided flex board, the route has 11 steps: copper cladding, die-cutting, drilling, through-hole copper plating, circuit formation, coverlay laminating, curing, surface treatment, filler lamination and punching, electrical testing, then inspection, packaging and shipping. The exact order can differ between manufacturers.
Why is the FPC fabrication process different from rigid PCB production?
Flex circuits use a polymer film instead of rigid glass epoxy, and a coverlay film instead of a printed solder mask. Parts are also handled on trays because the film is thin. These three differences add crease control, coverlay alignment and hole wall quality as key checkpoints.
What bend radius can a flexible PCB handle?
Bend radius depends on copper thickness, stack-up, coverlay and the number of bend cycles. Static bends can often use a tighter radius than dynamic flexing. Define the radius, cycle count and acceptance rule in a bend test per the approved plan, and use IPC-6013 and the relevant IPC-TM-650 methods as the reference framework. A common starting point for dynamic flex is a radius of several times the total stack thickness, but confirm it with a sample bend test.
What drives flexible PCB cost?
Material type, layer count, coverlay openings, stiffeners, surface finish, test coverage and yield all drive cost. Adhesiveless PI and fine-line etching cost more than adhesive-based static flex. A complex coverlay or rigid-flex transition adds lamination and test time. Ask for a cost breakdown by material, process and test so the design trade-offs are visible.
What affects flexible PCB yield?
Yield is most often lost to coverlay shift, lamination voids, delamination, adhesive squeeze-out, creases, etch variation and hole wall defects. Moisture control, plasma treatment, clean handling on trays and SPC on coverlay alignment and etch width are the main levers. A pilot run should measure these defect modes before volume release.
What is the typical lead time?
Lead time depends on layer count, tooling, material stock and test requirements. Prototype builds often take about 5 to 10 working days after data release, while volume runs typically take several weeks after tooling and sample approval. Confirm the schedule with the manufacturer before you commit the assembly plan.
How do I start a flexible PCB project with Gekunflex?
Send the stack-up, panel drawing and test plan first. The team reviews the build, confirms the process route and quotes the job. A sample is then approved before mass production, which keeps yield stable from prototype to volume.
Related Posts
- Flexible PCB SMT Process Guide — Related article
- PCB Lamination Process | Rigid & Flexible PCB Manufacturing Guide — Related article
- Flexible PCB: Features, Design Guide & Applications — Related article
- Closed-Loop Recyclable Flexible PCB Manufacturing Guide — Related article
- Flexible Circuit Board Assembly Equipment Design Guide — Related article